簡単な回答
Carbonyl iron powder is a very high-purity iron powder made by thermal decomposition of iron pentacarbonyl, producing fine particles with controlled morphology and excellent compressibility. It is chosen for additive manufacturing-adjacent and powder metallurgy applications because it offers uniform chemistry, strong magnetic response, reliable sintering behavior, and fine particle size control. In practice, it is most valuable in metal injection molding, soft magnetic components, microwave absorbers, welding consumables, and specialized feedstocks where purity, consistency, and compactability matter more than extreme high-temperature strength.
What Is Carbonyl iron powder
Carbonyl iron powder is a high-purity elemental iron powder produced through the carbonyl process rather than by conventional water atomization or gas atomization. In industrial terminology, it belongs to the iron powder family, but it occupies a distinctive niche because its value comes from chemistry control, very fine particle size, and a relatively smooth particle surface compared with many irregular reduced or water-atomized iron powders.
Historically, carbonyl iron developed as a specialty powder for electronics, magnetic materials, catalysts, powder metallurgy, and chemical applications where tight control of impurities was essential. The process makes it possible to generate iron particles from purified gaseous intermediates, which is why carbonyl powder is often associated with applications that cannot tolerate excessive oxygen, sulfur, or alloying contamination. That feature sets it apart from commodity iron powders used mainly for structural PM parts.
In additive manufacturing, Carbonyl iron powder is not the default powder for mainstream laser powder bed fusion in the same way spherical stainless steel or nickel superalloy powders are. Its importance is broader and more nuanced. It is frequently used in binder-based shaping, MIM feedstocks, magnetic composites, absorbers, and specialized research-grade feedstocks, while also appearing as a blending component in certain iron-based powder systems. For companies evaluating a wider iron-based powder portfolio, carbonyl grades are usually the fine, high-purity option rather than the lowest-cost bulk choice.
Carbonyl Iron Powder as a Specialty Iron Family
From a classification standpoint, carbonyl powder sits between traditional powder metallurgy feedstock and advanced functional powder. It can serve structural PM roles, but it is equally important in electromagnetic shielding, inductive materials, pharmaceutical iron supplementation, and radar-absorbent formulations. That breadth is unusual for an elemental metal powder.
Its relevance to additive manufacturing comes from process compatibility rather than from a single flagship AM route. Fine-particle feedstocks are useful in binder jetting research, extrusion-based metal feedstock development, metal injection molding, and hybrid manufacturing pathways that combine shaping with sintering. In those contexts, 高純度 and predictable sintering are often more important than the perfect spherical morphology demanded by high-speed powder-bed recoating.
Core Characteristics of Carbonyl Iron Powder
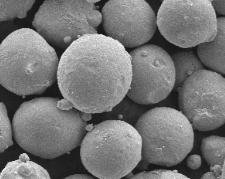
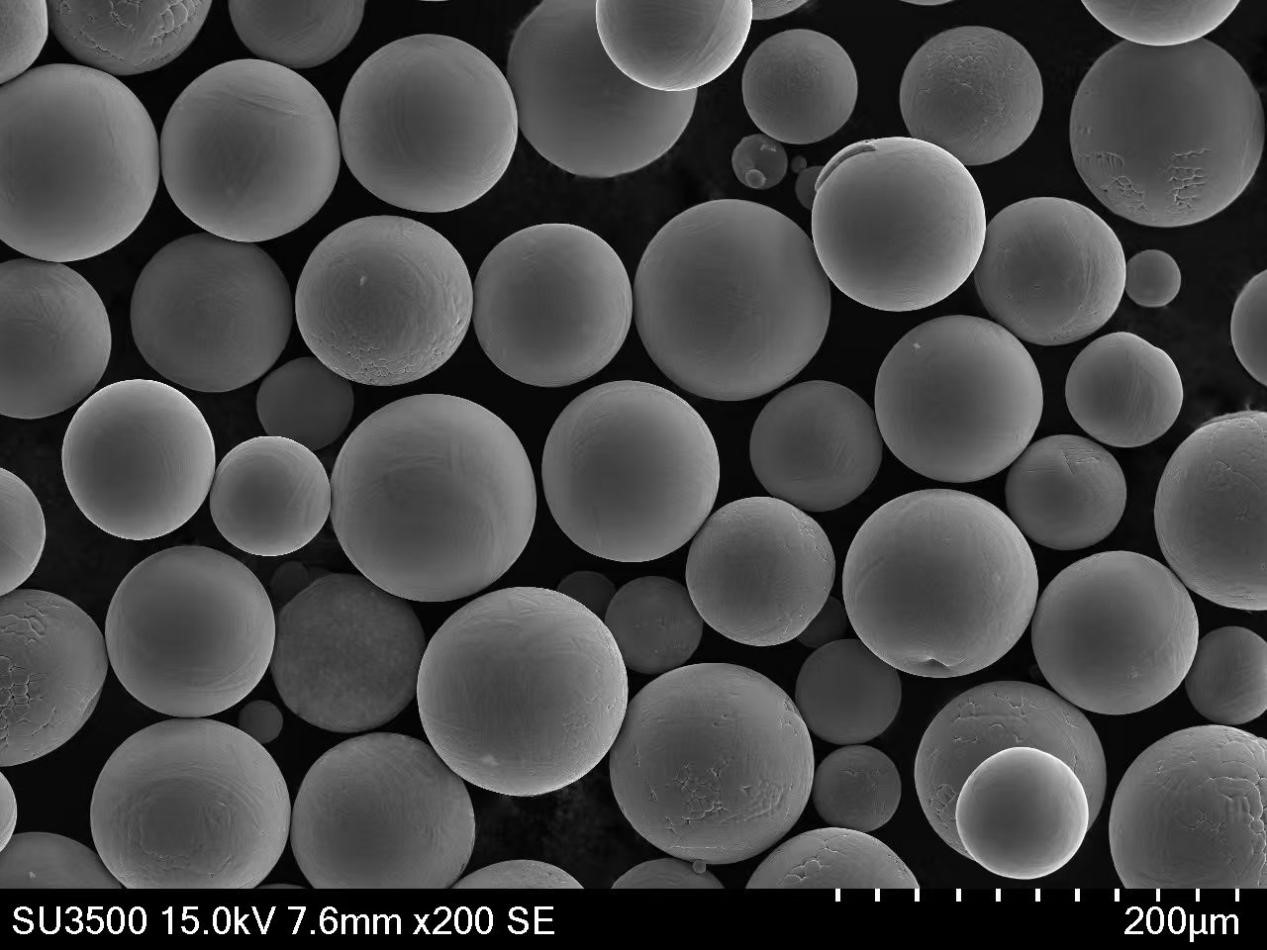
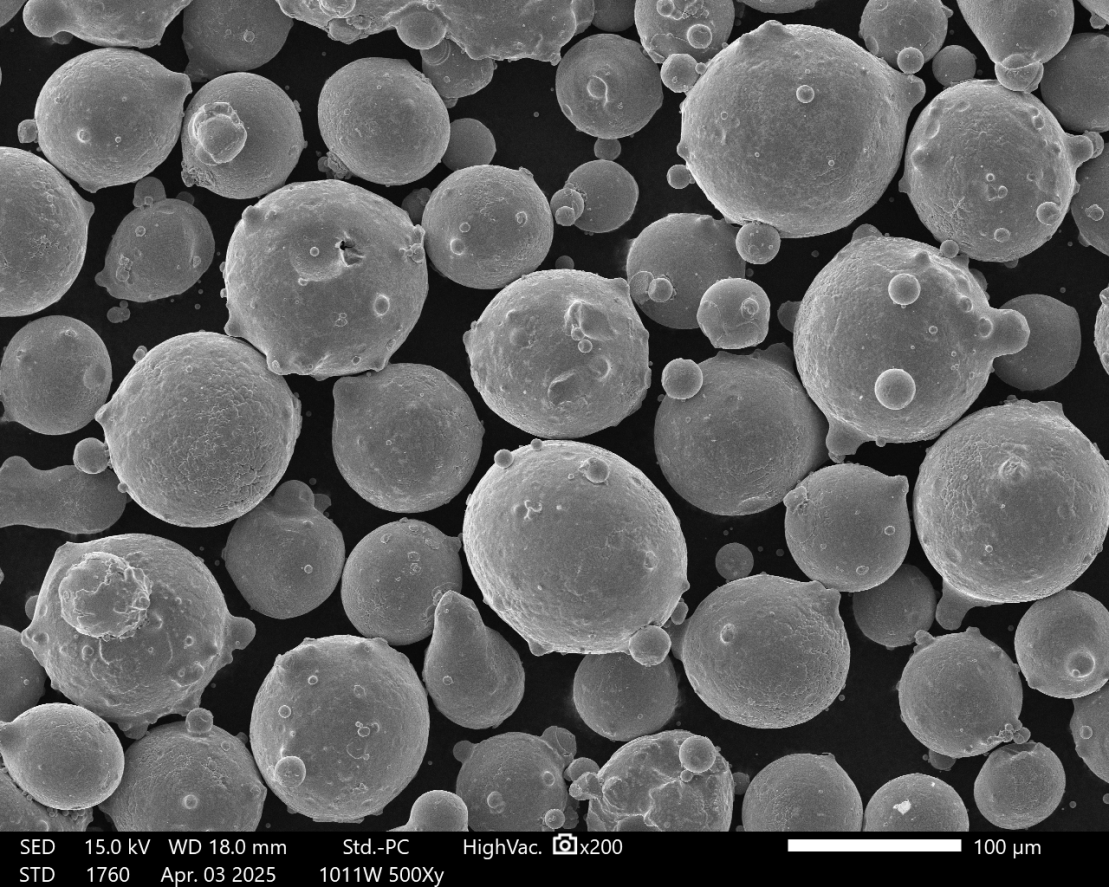
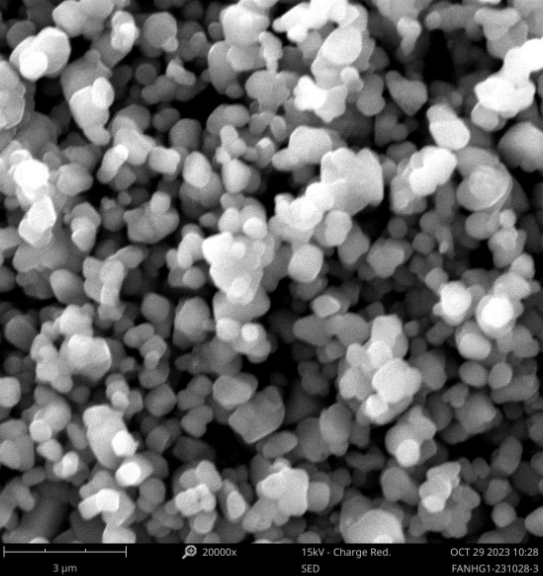
The most widely recognized characteristics are soft magnetic behavior, low impurity levels, fine and narrow PSD options, good green strength in compacted forms, and strong surface activity. Depending on the grade, the powder may be more onion-like, micro-spherical, or irregularly nodular than atomized powder, but it remains highly consistent when the decomposition conditions are controlled.
Carbonyl iron is often selected when particle uniformity and purity drive function, not just when iron is the cheapest metal available.
Why the Material Still Matters
The reason carbonyl iron remains commercially relevant is simple: not all powder applications reward the same attributes. A laser powder bed machine may prefer coarse, highly spherical particles, but magnetic absorbers, MIM feedstocks, and fine PM blends often perform better with very fine elemental iron. That is why Carbonyl iron powder continues to coexist with reduced, water-atomized, gas-atomized, and electrolytic iron products instead of being replaced by them.
化学組成
Although carbonyl iron powder is elemental iron, composition still matters because residual carbon, oxygen, nitrogen, sulfur, and trace metallic impurities affect magnetic permeability, compacting behavior, sinter density, and corrosion response. Commercial grades are therefore specified not only by iron content, but also by limits on residual elements and by the cleanliness of the production route.
Typical Carbonyl Iron Powder Composition
| Element / Constituent | Typical wt.% | Main Role or Origin | Functional Effect |
|---|---|---|---|
| フェ | 97.5-99.8 | ベースメタル | Determines magnetic response, sinterability, and elemental iron performance |
| C | 0.05-1.00 | Residual from carbonyl decomposition, grade dependent | Influences hardness, sintering response, and surface reactivity |
| O | 0.10-0.80 | Surface oxide from handling and passivation | Affects compressibility, magnetic loss, and reduction behavior during sintering |
| N | 0.01-0.50 | Residual gas pickup or process condition | Can affect aging behavior and, at higher levels, magnetic performance |
| S | 0.005 max | Impurity control target | Excess sulfur harms ductility and sintering cleanliness |
| Si | 最大0.05 | Trace impurity | Usually kept very low to preserve elemental purity |
| ムン | 最大0.05 | Trace impurity | Limited to avoid chemistry drift in specialty applications |
| P | 最大0.02 | 残留不純物 | Higher phosphorus can embrittle consolidated iron |
| 銅 | 最大0.05 | Trace metallic residual | Controlled for conductivity and magnetic consistency |
| Other metallic impurities | Supplier controlled, very low | Raw-material and equipment residuals | Influence reproducibility, especially in electronics-grade material |
The base iron content is the starting point, but it does not tell the whole story. Two carbonyl powders with similar iron content can behave differently if one has higher oxygen or carbon on the particle surface. This is especially relevant in magnetic and microwave applications, where loss behavior depends on both chemistry and microstructure.
Residual Carbon and Oxygen in Carbonyl Iron Powder
Carbon is not always undesirable in carbonyl iron. In some grades, a small amount is tolerated or even expected as a result of decomposition and subsequent conditioning. However, high residual carbon can alter sintering behavior and shift the properties of consolidated components away from those of near-pure iron.
Oxygen is equally important because the powder’s high surface area makes it naturally sensitive to oxidation. Fine powder offers excellent reactivity and sinterability, but the same surface area raises the need for careful passivation, packaging, and storage. For producers working across both carbonyl and spherical AM routes, these controls are just as important as the chemistry itself.
Why Purity Drives Performance
For soft magnetic uses, impurity control helps preserve permeability and minimize coercivity. For MIM and PM uses, it improves reproducibility during debinding and sintering. For shielding and absorber systems, it contributes to stable electromagnetic behavior from lot to lot. In other words, chemistry control is not merely a specification checkbox; it is the basis of how Carbonyl iron powder functions.
物理的および機械的特性
The properties of carbonyl iron should be separated into two categories: powder properties and consolidated-material properties. Powder properties determine flow, mixing, compaction, and feedstock behavior. Consolidated properties determine the performance of sintered or otherwise densified components. Because application routes differ widely, published values are usually expressed as typical ranges rather than single design numbers.
Typical Physical and Mechanical Properties
| プロパティ | 代表値 | 単位 | 試験基準 |
|---|---|---|---|
| 真の密度 | 7.86 | g/cm³ | Reference iron property data |
| 融点 | 1538 | °C | Reference iron property data |
| キュリー温度 | 770 | °C | Reference magnetic property data |
| Saturation magnetization | 210-220 | emu/g | Magnetic characterization methods |
| Apparent density of powder | 2.2-3.2 | g/cm³ | ASTM B212 |
| Tap density of powder | 3.0-4.8 | g/cm³ | Typical powder test practice |
| Microhardness of consolidated pure iron | 80-140 | HV | ASTM E92 or equivalent |
| Tensile strength of sintered compacts | 180-350 | MPa | ASTM E8/E8M on sintered material |
| Yield strength of sintered compacts | 100-220 | MPa | ASTM E8/E8M on sintered material |
| Elongation of sintered compacts | 5-20 | % | ASTM E8/E8M on sintered material |
| Thermal conductivity of iron | 70-80 | W/m-K | Reference iron property data |
The density and melting point are those of elemental iron, but powder-specific values such as apparent density vary strongly with morphology and grade. Fine carbonyl powder often has lower apparent density than coarser spherical powder because very small particles pack differently and experience stronger interparticle friction.
Magnetic and Thermal Behavior
For many users, the defining performance feature is magnetic rather than structural. Carbonyl iron displays strong soft-magnetic characteristics, making it useful in inductive materials, EMI shielding, and absorber systems. Its high saturation magnetization is one reason it remains relevant where ferrites lack enough magnetic loading and atomized powders are too coarse.
Thermally, iron conducts heat far better than nickel superalloys or titanium alloys, though not as well as copper. That makes it practical for sintered structural parts and feedstock systems where moderate heat transfer is useful but pure copper would be too soft or too conductive electrically.
Consolidated Strength and Sintering Behavior
Carbonyl iron powder is rarely chosen for peak tensile strength in the as-powder state; it is chosen for the way it densifies and consolidates. Fine particles shorten diffusion paths during sintering, which can improve bonding and help produce more uniform microstructures. In structural PM, it is often blended with alloying additions or lubricants to tune compressibility, shrinkage, and final mechanical performance.
When compared with coarser atomized feedstocks, carbonyl grades typically offer fine particle size and excellent compactability, though handling becomes more demanding because dusting, oxidation sensitivity, and flow issues increase as particles get smaller.
仕様および取り扱いグレード
Commercial Carbonyl iron powder is sold by particle size, purity level, morphology class, and end-use grade. Some grades are optimized for PM pressing; others are designed for magnetic applications, microwave absorption, MIM, coating, or chemical use. The most important procurement variables are PSD, oxygen level, apparent density, tap density, and whether the powder is passivated or surface treated.
Typical Grade Windows and Particle Size Ranges
| 学年/PSDクラス | 代表的なPSD範囲 | 見かけ密度 | タップ密度 | ホールの流れ | 酸素含有量 | Sphericity / Shape | Grade Cross-Reference |
|---|---|---|---|---|---|---|---|
| Ultrafine electronic grade | 1-5 µm | 2.2-2.8 g/cm³ | 3.0-3.8 g/cm³ | Often not measurable by Hall | 0.20-0.80 wt.% | Fine, rounded to nodular | Custom supplier grade; purity-focused |
| Fine PM / MIM grade | 3-10 µm | 2.3-3.0 g/cm³ | 3.2-4.2 g/cm³ | Slow or not applicable | 0.15-0.60 wt.% | Fine, uniform | Internal PM/MIM grade mapping |
| Medium carbonyl grade | 10-45 µm | 2.5-3.2 g/cm³ | 3.5-4.8 g/cm³ | 18-35 s/50 g typical | 0.10-0.40 wt.% | Rounded to near-spherical | Used in blends and specialty shaping |
| Coarser specialty cut | 15-53 µm | 2.6-3.3 g/cm³ | 3.6-4.9 g/cm³ | 16-30 s/50 g typical | 0.10-0.35 wt.% | More free-flowing | Custom screened grade |
| Standards reference set | Testing per ASTM B212 apparent density and ASTM B213 Hall flow; terminology aligned with ISO/ASTM 52900 where AM context applies | - | - | - | - | - | ASTM / ISO / DIN / GB references are generally test-method based rather than a single universal carbonyl iron grade standard |
Unlike standard LPBF nickel or titanium powders, carbonyl iron grades are not usually purchased under one universally recognized AM alloy designation. Instead, buyers specify the powder by function: electromagnetic use, PM pressing, MIM feedstock, absorber filler, or research-grade additive manufacturing blend. That makes supplier datasheets and acceptance criteria particularly important.
規格および試験方法
Because the product is often application-specific, testing standards matter more than one single alloy specification. Apparent density is commonly evaluated under the [ASTM B212 apparent density standard], while flow may be assessed using the [ASTM B213 Hall flow standard] when particle size is coarse enough for the method to be meaningful. For very fine powders, other flow and rheology methods may be more informative than Hall flow.
In additive-manufacturing-related work, terminology around feedstocks, build routes, and post-processing is aligned with the [ISO/ASTM 52900 additive manufacturing vocabulary]. However, Carbonyl iron powder is still more often specified as a specialty iron powder than as a mainstream powder-bed-fusion material.
Available Grades in Practice
Typical market grades include untreated carbonyl iron, passivated carbonyl iron, reduced-oxygen carbonyl iron, magnetic-grade carbonyl iron, and particle-size-tailored cuts for MIM or blending. Some suppliers also offer compounded forms for absorber systems or coated grades for dielectric tuning. Where application overlap exists, users may compare these options with spherical feedstocks from a broader metal powder applications catalog to decide whether a part is better suited to PM, MIM, DED, or another route.
製造工程
The manufacturing route is the single biggest factor separating carbonyl iron from most other iron powders. The classic production path is the carbonyl process, in which iron reacts with carbon monoxide to form iron pentacarbonyl, followed by controlled thermal decomposition into fine iron powder. That route creates a powder with unusually high purity and fine size, but it is not the most economical way to make bulk iron powder.
Powder-Making Route Comparison
| プロセス | 球形度 | 酸素ピックアップ | PSDコントロール | スループット | 相対的なコスト |
|---|---|---|---|---|---|
| Carbonyl decomposition | Moderate to high, very uniform fine particles | Low during controlled decomposition, but fine powder is oxidation-sensitive after production | Excellent in fine ranges | ミディアム | 高い |
| ガスアトマイズ(GA) | High for suitable melts | 低~中程度 | グッド | 高い | 中程度 |
| VIGA / EIGA | 非常に高い | Low to very low | 非常に良い | ミディアム | 高い |
| 準備 | 非常に高い | 非常に低い | Good, often coarser and cleaner | Medium to low | 高い |
Carbonyl Decomposition Route
In the carbonyl process, iron-bearing feedstock is converted into iron pentacarbonyl under controlled pressure and temperature. The volatile carbonyl compound is purified and then decomposed thermally, depositing elemental iron as fine particles while releasing carbon monoxide for recovery or recirculation. The resulting powder is then passivated, classified, and packaged.
This route is attractive because it starts from a gaseous intermediate, which helps remove many contaminants before powder formation. That is why Carbonyl iron powder can achieve very high purity and exceptionally fine, consistent particle sizes. The main drawbacks are process complexity, safety requirements, and higher manufacturing cost than commodity atomized or reduced powders.
How Carbonyl Iron Differs from GA, VIGA, EIGA, and PREP
GA, VIGA, EIGA, and PREP are melt-based routes. They are ideal when the market wants spherical particles for recoating, high flowability, or advanced superalloy and titanium AM systems. Carbonyl processing is not built around those priorities; it is built around purity and fine powder generation.
That difference explains why carbonyl iron is not usually the first answer for LPBF machines. Even though melt-based methods can produce cleaner and more spherical powders for many AM metals, carbonyl decomposition remains preferable when the application values controlled decomposition process benefits such as ultrafine particle size and narrow chemistry control.
Post-Processing and Powder Conditioning
After primary production, the powder may be reduced, annealed, classified, blended, passivated, or surface modified. These steps can change the apparent density, oxidation level, and compaction behavior substantially. In high-performance PM or electronics work, the conditioning stage can be as important as the initial decomposition step because end-use performance depends on stable lot-to-lot behavior, not just nominal purity.
業界別の用途
Carbonyl iron powder serves a wider range of industries than its name alone suggests. Its most natural applications sit at the intersection of powder metallurgy, electronics, magnetics, coatings, and specialty manufacturing rather than exclusively in one AM process.
Powder Metallurgy and MIM
In PM and MIM, carbonyl iron is used where very fine particles improve binder loading, sintering kinetics, and dimensional control. The powder can be used alone for near-pure iron components or as a base constituent in alloyed feedstocks. Its fine size also helps fill interstitial spaces when blended with coarser iron powders, improving packing behavior in some formulations.
For complex small parts, the material is especially useful in feedstocks requiring uniform dispersion and predictable shrinkage. This is one reason it still appears in advanced shaping systems even though spherical gas-atomized powders dominate many premium AM headlines.
Soft Magnetic and EMI Applications
Carbonyl iron is widely used in inductors, magnetic composites, EMI shielding materials, and microwave absorbers. The combination of high saturation magnetization, controlled purity, and fine particle sizing makes it attractive for radio-frequency and electromagnetic management systems. In these applications, performance depends as much on particle morphology and coating strategy as on nominal iron content.
Welding, Thermal Spraying, and Surface Engineering
Certain grades are used in welding consumables, surfacing powders, and spray feedstocks. Pure or near-pure iron additions can help tailor deposit chemistry, especially in repair or build-up systems where a low-alloy ferrous response is desired. In surface engineering, carbonyl iron may also serve as a functional filler rather than the main structural material.
Chemical, Medical, and Consumer Uses
Outside engineering structure, carbonyl iron is used in catalysts, laboratory reagents, nutritional iron formulations, and specialty polymer-filled systems. Pharmaceutical-grade carbonyl iron is selected because of its purity and controlled particle behavior, though those grades are governed by very different qualification logic than industrial PM powders.
Shanghai Truer’s broader manufacturing ecosystem includes PM, MIM, laser cladding, DED, and spherical ferrous materials, so Carbonyl iron powder fits most naturally into the company’s ferrous and hybrid processing landscape rather than only into powder-bed fusion. Readers comparing it with stainless, titanium, or other specialty feedstocks can use the wider company background overview to understand how different powder routes connect to different end-use processes.
代替材料との比較
Material selection depends on the end function. Carbonyl iron is excellent when purity, magnetics, and fine particle behavior dominate; it is less competitive when corrosion resistance, flowability for powder-bed fusion, or very low cost are the main objectives. The best comparison is therefore not with only one metal, but with several common alternatives.
Carbonyl Iron Powder vs Other Metal Powder Options
| 素材 | 密度 (g/cm³) | Main Strengths | Printability / Process Fit | 耐食性 | 相対的なコスト |
|---|---|---|---|---|---|
| Carbonyl iron powder | 7.86 | High purity, magnetic performance, fine PSD, good sinterability | Best for PM, MIM, blends, absorbers; limited for mainstream LPBF | Low to moderate unless protected or alloyed | 中~高 |
| Water-atomized iron powder | 7.86 | Low cost, good compressibility for PM | Excellent for conventional PM, weaker for high-end AM due to irregular shape | 低~中程度 | 低い |
| Gas-atomized stainless steel powder | 7.7-8.0 | Spherical flowability, corrosion resistance, AM readiness | Strong fit for LPBF and binder jetting | Good to excellent | 中~高 |
| Carbonyl nickel powder | 8.9 | Corrosion resistance, conductivity, catalytic performance | Good for specialty PM and batteries; less magnetic than iron | グッド | 高い |
| Soft magnetic ferrite powder | ~4.8-5.3 | High resistivity, low eddy current loss | Strong for RF magnetic ceramics, not a structural metal PM powder | Excellent chemical stability in many environments | ミディアム |
Compared with water-atomized iron, carbonyl powder is cleaner and finer but more expensive. Compared with stainless steel AM powder, it gives up corrosion resistance and powder-bed flowability in exchange for purity and magnetic functionality. Compared with carbonyl nickel, iron is usually more economical and more strongly magnetic, although nickel can outperform it in corrosion-sensitive chemical systems.
This comparison also shows why Carbonyl iron powder is best understood as a functional iron powder rather than as a direct one-for-one substitute for every AM feedstock. It wins when particle-scale behavior matters.
当社
Shanghai Truer Technology Co., Ltd., operating am-printing.com, was established in 2009 and created its additive manufacturing business in 2019. The company works across metal powder equipment and powder supply, including Selective Electron Beam Melting equipment, Plasma Rotating Electrode Process powder-making equipment, and gas atomization-related capabilities. Its powder portfolio includes TiNi, TiTa, TiAl, TiNbZr, CoCrMo, and broader nickel-based, cobalt-based, titanium-based, copper-based, aluminum-based, and stainless steel spherical metal powders, serving SLM, SEBM, DED, laser cladding, powder metallurgy, MIM, HIP, spraying, welding, and coating applications in sectors such as 3C electronics, hand tools, remote control cars, medical, aerospace, and nuclear power. Technical discussions on powder selection and process matching can be routed through the powder supply contact channel.
よくあるご質問
Q1. Is Carbonyl iron powder used in metal 3D printing?
Yes, but not usually as the first-choice feedstock for mainstream laser powder bed fusion. Carbonyl iron powder is more commonly used in binder-based shaping, MIM feedstocks, PM blends, absorber materials, and research applications where ultrafine purity-controlled iron is more valuable than highly spherical recoating behavior.
Q2. Why is Carbonyl iron powder considered high purity?
It is made through a gaseous intermediate, iron pentacarbonyl, which allows purification before decomposition into elemental iron particles. That process route helps minimize many metallic contaminants compared with some conventional iron powder production methods.
Q3. What particle size is typical for Carbonyl iron powder?
Commercial grades often range from about 1 µm up to 45 µm or slightly coarser screened cuts, depending on the application. Ultrafine grades are common in electronics and absorber systems, while somewhat coarser grades are used in PM, MIM, and specialty feedstock blending.
Q4. Is Carbonyl iron powder magnetic?
Yes. Carbonyl iron powder is strongly ferromagnetic and is valued for soft-magnetic applications because it offers high saturation magnetization and useful electromagnetic performance when properly processed or coated.
Q5. How does Carbonyl iron powder compare with atomized iron powder?
Carbonyl iron powder is generally finer, purer, and more functionally specialized, while atomized iron powder is usually cheaper and better suited to large-volume structural PM. Atomized powders also tend to offer better flow in coarser size ranges, especially when they are gas-atomized and spherical.
Q6. Does Carbonyl iron powder resist corrosion well?
Not especially when compared with stainless steels, nickel alloys, or cobalt alloys. Because it is essentially pure iron, it usually needs alloying, coating, controlled atmospheres, or protective system design if the final application involves moisture, salts, or aggressive chemicals.