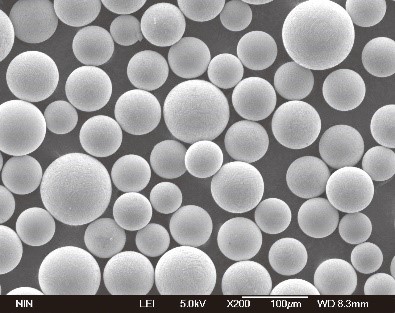
簡単な回答
Spherical pure Co powder is high-purity cobalt metal powder engineered with near-spherical particle morphology for reliable flow and packing in advanced powder-based manufacturing. It is chosen for additive manufacturing and related powder-processing routes when users need strong thermal stability, controlled magnetic behavior, high-temperature performance, and consistent spreading in laser, electron beam, or sinter-based workflows. In practice, it is most valuable for specialty research parts, wear-facing deposits, magnetic components, alloy development, and cobalt-rich feedstock systems where purity and particle shape directly affect print consistency.
What Is Spherical pure Co powder
Spherical pure Co powder is a cobalt metal powder whose primary constituent is elemental cobalt rather than a cobalt-base alloy such as CoCrMo or Stellite-type compositions. The term “spherical” refers to particle morphology produced by atomization or related melt-based powder-making methods, while “pure” indicates that cobalt content is intentionally kept high and residual elements are tightly controlled. In metal AM, that combination matters because morphology governs powder behavior and chemistry governs how the powder melts, solidifies, sinters, or reacts with other elements.
Within the broader cobalt materials family, pure cobalt powder occupies a more specialized niche than cobalt-chromium medical or wear-resistant alloys. It is not the default cobalt feedstock for every part; instead, it is used where the designer wants cobalt’s intrinsic properties without the full chemistry package of chromium, molybdenum, tungsten, or nickel additions. That makes it relevant in feedstock development, magnetic and functional materials, thermal spray, hardfacing blends, and selected additive manufacturing projects.
Spherical pure Co powder in the cobalt materials family
Cobalt-based materials are usually discussed through their alloys because alloys dominate commercial part production. Pure cobalt, however, remains important because it acts as a baseline composition, a master feedstock for alloy development, and a functional material in its own right. Engineers evaluating a cobalt alloy powder range often compare pure cobalt with CoCrMo or hardfacing grades to determine whether corrosion resistance, wear resistance, or simpler chemistry is more important.
One reason cobalt behaves differently from neighboring metals is its crystal structure. At room temperature, cobalt is generally hexagonal close-packed, while at higher temperature it can transform toward a face-centered cubic structure. This allotropic phase behavior affects deformation, thermal response, and microstructural development during rapid melting and cooling.
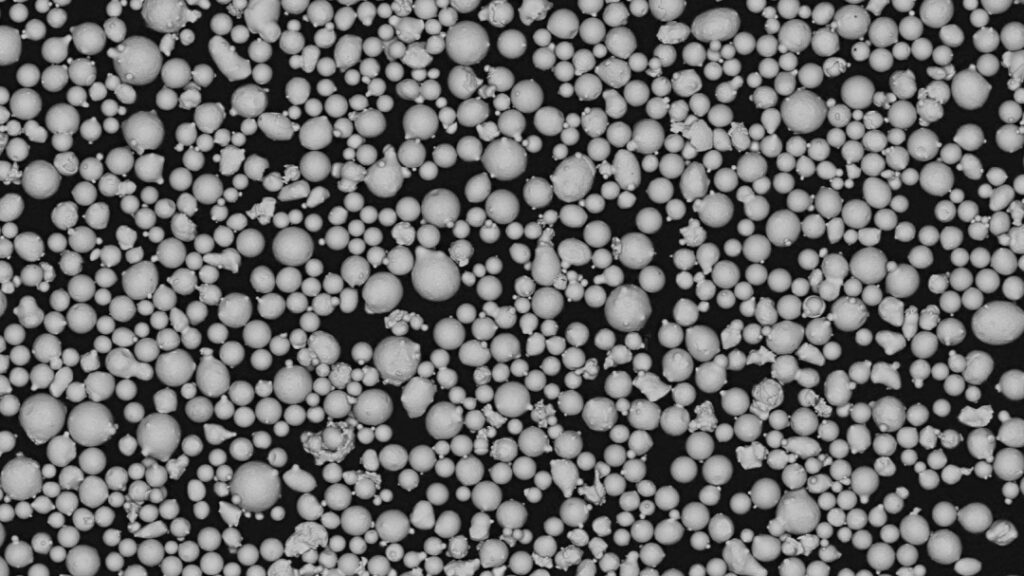
Why spherical morphology matters
Shape is not a cosmetic attribute in powder processing. Spherical particles generally flow more consistently, spread more evenly in recoating systems, and pack with fewer voids than irregular particles. That is why AM users often prioritize high sphericity and low oxygen even before they fine-tune laser power, scan strategy, or post-processing conditions.
Spherical powder also tends to generate more stable apparent density and better repeatability in automated feeding systems. Whether the process is laser powder bed fusion, electron beam melting, DED, MIM, or HIP canning, consistent particle motion is a major contributor to stable manufacturing.
Where pure cobalt differs from cobalt alloys
Pure cobalt lacks the built-in corrosion resistance of high-chromium cobalt alloys and the solid-solution complexity of nickel superalloys. What it offers instead is simpler chemistry, cobalt-dominant magnetic and thermal behavior, and flexibility as a starting point for custom alloying. For developers working on new cobalt-rich formulations, using pure cobalt powder can be a cleaner route than diluting a multi-element alloy.
In powder-based manufacturing, the value of pure cobalt is not that it replaces every cobalt alloy; it is that it gives engineers a controllable cobalt-rich starting point.
Industrial context
Historically, cobalt has been important in high-temperature alloys, cutting and wear systems, magnets, batteries, and surface engineering. In additive manufacturing, pure cobalt is less common than stainless steels, titanium alloys, or nickel superalloys, but it still attracts interest where powder purity, functional response, and custom chemistry matter more than commodity volume. That is particularly true in R&D environments, specialized DED repairs, alloy prototyping, and advanced sinter-based cobalt components.
化学組成
The chemistry of spherical pure Co powder is straightforward in principle but demanding in practice. The target is a cobalt-rich composition with very low residuals, because impurities such as oxygen, carbon, sulfur, and iron can affect melt behavior, phase stability, ductility, magnetic response, and final density. As with most high-value AM powders, the certificate of analysis matters as much as the nominal product name.
Typical composition of spherical pure Co powder
| Element / Constituent | Typical wt% | Main Metallurgical Role | Effect on Processing and Performance |
|---|---|---|---|
| Co | ≥99.5 | 非金属マトリックス | Governs cobalt-specific thermal, magnetic, and high-temperature behavior |
| O | 0.02–0.15 | Surface oxide indicator | Higher oxygen can reduce ductility, worsen fusion, and increase inclusion risk |
| C | ≤0.05 | Residual control | Excess carbon can form carbides or alter hardness and solidification response |
| フェ | ≤0.20 | Common metallic residual | Can shift magnetic and mechanical behavior if concentration rises |
| ニー | ≤0.20 | Metallic residual or alloy trace | May change phase stability and soften cobalt-dominant behavior slightly |
| Si | ≤0.05 | Deoxidation-related residual | Elevated silicon can affect cleanliness and brittle phase formation |
| ムン | ≤0.05 | Minor residual | Limited effect at low levels, but excessive levels complicate chemistry control |
| S / P | ≤0.02 each | Impurity control | Higher sulfur or phosphorus can reduce hot workability and toughness |
The first thing to notice is that cobalt content alone does not define powder quality. A cobalt assay above 99.5 wt% is valuable, but oxygen and carbon are often more predictive of how the powder will behave under a laser or in a sintering furnace. In high-surface-area powders, even small changes in interstitial content can affect porosity, fusion continuity, and fracture behavior.
Role of cobalt as the dominant element
Cobalt brings a distinctive combination of density, elevated melting temperature, magnetic response, and high-temperature phase stability. It also acts as a robust matrix for future alloying, which is why pure cobalt powder is often used in development programs before chromium, tungsten, molybdenum, or nickel are introduced in deliberate amounts. In that sense, pure cobalt is not just a final material but also a platform chemistry.
Why impurity limits matter in AM powder
Oxygen is especially important because oxide films can persist on particle surfaces and interfere with clean metallurgical bonding. Carbon matters because it can unintentionally push the material toward carbide formation if the process environment or binder system contributes additional carbon. Iron and nickel are not always harmful in trace amounts, but they can shift the response away from a true cobalt baseline.
Chemistry control for research and production
Users purchasing spherical pure Co powder for research often ask for even tighter residual limits than users buying it for thermal spray or blend feedstock. That is because experimental alloy development depends on starting from a well-defined composition. In a production environment, feedstock purity also supports more repeatable parameter development, especially when the same powder is expected to perform across multiple batches.
物理的および機械的特性
Property discussions for pure cobalt require one important caution: the numbers for loose powder are not the same as the numbers for a dense printed, sintered, or hot-isostatically pressed part. Powder users should separate feedstock properties such as flow and apparent density from bulk material properties such as tensile strength, hardness, and thermal conductivity. The values below are therefore typical ranges for spherical powder and consolidated pure cobalt, not a single fixed specification for every process state.
Typical physical and mechanical properties of spherical pure Co powder and consolidated cobalt
| プロパティ | 代表値 | 単位 | 試験規格/試験条件 |
|---|---|---|---|
| 真の密度 | 8.8–8.9 | g/cm³ | Typical pure cobalt value |
| 見かけ密度 | 4.6–5.4 | g/cm³ | Typical spherical powder, ASTM B212 context |
| 融点 | 1495 | °C | Pure cobalt nominal value |
| ホールの流れ | 12–20 | s/50 g | Typical spherical AM-grade powder, ASTM B213 context |
| 降伏強度 | 250–500 | MPa | Typical consolidated cobalt, condition dependent |
| 引張強度 | 450–900 | MPa | Typical consolidated cobalt, processing dependent |
| 伸び | 8–30 | % | Typical dense material, microstructure dependent |
| 硬度 | 120–260 | HV | Typical consolidated cobalt |
| 熱伝導率 | 70–100 | W/m-K | Typical bulk cobalt range |
| キュリー温度 | about 1120 | °C | Magnetic transition reference |
Pure cobalt is dense, thermally stable, and relatively high melting compared with aluminum or copper alloys. Those characteristics can be useful in high-heat environments, but they also mean process energy density must be tuned carefully. In laser-based systems, too little energy leads to incomplete fusion, while too much can increase evaporation, spatter, or instability.
Mechanical behavior after consolidation
Mechanical properties vary strongly with process route. A dense HIPed specimen, a laser-remelted coupon, and a conventionally sintered part can all begin with similar powder yet finish with different grain structures and defect populations. That is why cobalt property data should be treated as process-dependent rather than universal.
Pure cobalt is often stronger than users expect, especially after rapid-solidification routes that create fine microstructures. At the same time, ductility can be sensitive to oxygen pickup, grain boundary cleanliness, and thermal history, so post-processing often plays a bigger role than with easier-printing materials like 316L.
Thermal and magnetic performance
Cobalt remains attractive in functional applications because it combines respectable thermal conductivity with persistent magnetic behavior at elevated temperature. Its Curie temperature is much higher than that of many iron-based soft magnetic materials, which can matter in specialized sensors, actuators, and high-temperature electromagnetic systems. This is one reason pure cobalt is sometimes chosen over iron-based powder grades when thermal resilience and cobalt chemistry are central to design intent.
Powder behavior in AM equipment
For feedstock users, the most practical property is often not tensile strength but powder spreadability. A spherical cobalt powder with narrow PSD and low satellites usually recoats more consistently than irregular cobalt particles. In production terms, powder flowability and layer uniformity can determine whether a theoretically excellent material actually becomes a stable manufacturing material.
仕様および取り扱いグレード
Unlike highly codified aerospace titanium grades, pure cobalt powder is usually sold through a combination of internal supplier specifications, particle size classes, chemistry thresholds, and morphology requirements. The exact grade naming system varies by producer, but buyers typically focus on three questions: how pure the cobalt is, how spherical the particles are, and what PSD is optimized for the target process. Those questions matter whether the user is printing, spraying, molding, or blending.
Typical grades and specification windows
| Supply Grade / Condition | PSDレンジ | 見かけ密度 | タップ密度 | ホールの流れ | Oxygen / Sphericity / Cross-Reference |
|---|---|---|---|---|---|
| Co-AM15-45 | 15-45 µm | 4.7–5.3 g/cm³ | 5.2–5.9 g/cm³ | 13~19秒/50 g | O typically 0.02–0.08 wt%; high sphericity; LPBF / MIM oriented |
| Co-AM15-53 | 15–53 µm | 4.6~5.2 g/cm³ | 5.1~5.8 g/cm³ | 12–18 s/50 g | O typically 0.02–0.10 wt%; broad AM utility grade |
| Co-DED45-105 | 45-105 µm | 4.8~5.4 g/cm³ | 5.3–6.0 g/cm³ | 11–17 s/50 g | O typically 0.02–0.10 wt%; good feed behavior for DED |
| Co-SP53-150 | 53-150 µm | 4.9~5.5 g/cm³ | 5.4~6.1 g/cm³ | 10–16 s/50 g | O typically 0.03–0.12 wt%; thermal spray or cladding grade |
| Standards / Test Context | - | ASTM B212 | ASTM B527 | ASTM B213 | Chemistry to supplier or customer spec; AM terminology aligned with ISO/ASTM 52900 積層造形用語集 |
The most common AM-related cuts are 15–45 µm and 15–53 µm because they suit powder bed processes and fine-powder development work. DED and thermal spray tend to use coarser ranges because the powder must feed through nozzles rather than form extremely thin layers. In either case, sphericity and satellite control matter because they affect flow consistency and apparent density.
Spherical pure Co powder for LPBF and DED
For LPBF, a narrower PSD helps produce smooth layers and predictable absorption behavior. For DED, the optimum range is usually broader and coarser because the powder must travel through a carrier-gas stream and enter a melt pool efficiently. This is why the same chemistry can be sold in multiple PSD cuts without changing the underlying cobalt purity target.
Standards context and test methods
Powder suppliers often rely on general metal-powder methods instead of cobalt-specific AM standards. Flow can be assessed using the ASTM B213 Hall flow standard, and apparent density is commonly framed with the ASTM B212 apparent density standard. These do not certify end-use success by themselves, but they provide a common language for comparing lots.
What buyers should ask for
A technical data package should include chemistry, PSD, oxygen, apparent density, tap density, Hall flow, and SEM morphology if available. Some buyers also request laser diffraction curves, ICP results, and reuse guidance. That is particularly sensible with cobalt because small chemistry drifts can materially change both print behavior and downstream performance.
製造工程
The production route used for spherical pure Co powder largely determines whether the feedstock is suitable for premium additive manufacturing or only for less demanding processes. Melt atomization methods are favored because they create rounder particles with better flow, while mechanical methods are generally less suitable for high-end AM. In cobalt, process atmosphere control is especially important because oxygen pickup can undermine the benefit of starting from a high-purity metal.
Comparison of cobalt powder manufacturing routes
| プロセス | 球形度 | 酸素ピックアップ | PSDコントロール | スループット | 相対的なコスト |
|---|---|---|---|---|---|
| ガスアトマイズ(GA) | 高い | 低~中程度 | グッド | 高い | ミディアム |
| 準備 | 非常に高い | 非常に低い | グッド | ミディアム | 高い |
| VIGA | 高い~非常に高い | 低い | 非常に良い | ミディアム | 高い |
| EIGA | 非常に高い | 非常に低い | 非常に良い | ミディアム | 高い |
| Plasma Atomization / Related Plasma Routes | 非常に高い | 低い | 良い~非常に良い | 低~中 | 高い |
Gas-atomized spherical pure Co powder
Gas atomization is the most broadly practical route for commercial cobalt powder. Molten cobalt is disintegrated by high-pressure inert gas, producing droplets that solidify into predominantly spherical particles. The route offers a strong balance of cost, throughput, and morphology, which is why many AM-grade cobalt powders begin here.
For pure cobalt, inert handling is critical because oxidation during melting, atomization, or collection can raise oxygen beyond desirable AM levels. Proper sieving and fines removal are also important because excess fines may increase oxygen content and reduce powder bed stability.
PREP and premium spherical cobalt feedstock
PREP is often associated with reactive or high-value alloys, but it is also relevant when exceptionally spherical cobalt powder is required. A rotating electrode is melted at the tip, and centrifugal forces eject droplets that solidify into smooth particles with low contamination. The main advantage is powder cleanliness and shape; the main drawback is cost and lower throughput versus large-scale gas atomization.
VIGA and EIGA in cobalt powder production
Vacuum induction gas atomization and electrode induction gas atomization are useful when tighter atmosphere control and improved cleanliness are priorities. These routes can reduce contamination and improve lot consistency, especially for advanced AM development. In cobalt, that can be important for research powders or when downstream qualification is sensitive to subtle chemistry changes.
Trade-offs between route, cost, and performance
No manufacturing route is universally best. If the target application is thermal spray or a less sensitive cladding operation, a slightly broader PSD from GA may be perfectly appropriate. If the powder is destined for precision LPBF parameter development or specialty research, the value of 高温安定性 may only be realized if morphology, oxygen, and impurity levels are held to correspondingly high standards.
業界別の用途
Spherical pure Co powder is not a mass-market general-purpose AM material. Its industrial relevance comes from specialized functions where cobalt itself—not just any cobalt alloy—delivers the needed thermal, magnetic, or alloy-design behavior. That makes its application map narrower than stainless steel but deeper in high-value technical niches.
Aerospace, energy, and high-heat systems
Pure cobalt powder is useful as a precursor or constituent in high-temperature coatings, repair deposits, and experimental cobalt-rich structures for demanding thermal environments. In aerospace and energy settings, it may appear in DED development programs, cladding layers, or alloy prototyping where cobalt’s hot-strength baseline is needed before chromium, tungsten, or nickel additions are optimized. Users comparing it with a nickel-based powder lineup typically do so when deciding between oxidation resistance, hot-corrosion behavior, and alloy-design flexibility.
Medical and dental materials development
Medical production more commonly uses CoCrMo than pure cobalt, especially for implantable or wear-critical applications. Even so, pure cobalt powder can still be relevant in research, precursor blending, and functional studies tied to cobalt-rich systems. In that context it serves more as a controlled input material than as a direct implant-grade final alloy.
Electronics, magnetic parts, and precision devices
Cobalt’s magnetic persistence at elevated temperature gives it value in sensors, actuators, electromagnetic assemblies, and specialty precision devices. When powders are processed by MIM, binder jetting, or fine AM routes, particle shape becomes crucial to homogeneous filling and sintering. This is one area where pure cobalt differs meaningfully from many materials in the industrial application sectors commonly served by general AM powders.
Tooling, wear surfacing, and thermal spray
Cobalt has a long history in wear-related materials, and pure cobalt powder is often used as a base input for coatings, overlays, and cobalt-rich blends. In laser cladding and thermal spray, spherical morphology supports consistent feeding and deposition efficiency. That makes pure cobalt an attractive feedstock not because it is fully optimized out of the box, but because it is a controllable cobalt-rich starting point.
Research alloys and multi-material development
Universities, national labs, and R&D teams often use pure cobalt powder for alloy prototyping, especially when exploring magnetic materials, medium-entropy systems, and custom AM compositions. In these programs, starting with a high-purity spherical cobalt source reduces uncertainty and makes it easier to interpret how later additions affect microstructure. Compared with a refractory metal powder portfolio, cobalt offers a different balance of density, melting behavior, and processability for such development work.
代替材料との比較
Pure cobalt is rarely the only candidate on an engineer’s shortlist. It is usually evaluated against cobalt-chromium, pure nickel, nickel superalloys, and in some cases tungsten-containing materials depending on whether the part prioritizes magnetics, corrosion resistance, heat resistance, or wear. The best choice depends on whether the project values compositional simplicity or application-ready alloy performance.
Spherical pure Co powder versus alternative AM powders
| 素材 | 密度 (g/cm³) | Main Advantage | 相対的なコスト | Printability / Process Fit | Corrosion / Service Profile |
|---|---|---|---|---|---|
| Spherical pure Co powder | 8.8–8.9 | High-purity cobalt matrix, magnetic and thermal functionality, alloy-design flexibility | 高い | Good in DED, MIM, HIP, research AM; more niche in LPBF | Moderate oxidation and corrosion behavior unless further alloyed |
| CoCrMo粉末 | 8.3–8.5 | Strong wear resistance, corrosion resistance, mature medical and dental use | 高い | Excellent for LPBF and established cobalt-alloy workflows | Better corrosion and wear performance than pure cobalt |
| Pure Ni powder | 8.9 | Good ductility, corrosion performance, and alloying base chemistry | ミディアムハイ | Good across spray, PM, and selected AM routes | Better general corrosion resistance than pure cobalt |
| Ni-based superalloy powder | 8.1–8.5 | Strong high-temperature oxidation and creep resistance | 高い | Highly mature in AM for aerospace and energy | Excellent elevated-temperature service profile |
| W-containing cobalt or hardfacing alloy powder | 8.5–9.5 | Superior wear and hot-hardness performance | 高い | Best for cladding, overlays, and wear applications | Service-focused rather than pure-material flexibility |
Compared with CoCrMo, pure cobalt is simpler but less application-ready. Compared with pure nickel, cobalt offers different magnetic and hot-structure behavior but often at a higher raw-material cost and with less widespread printing data. Against nickel superalloys, pure cobalt usually loses on oxidation resistance and qualification maturity, but it can still win when cobalt-dominant functionality is the primary design driver.
When spherical pure Co powder is the right choice
It is the right choice when the part or experiment needs cobalt itself rather than a pre-engineered cobalt alloy. That includes precursor blending, magnetic-function studies, cobalt-rich cladding, and AM material development where chemistry must remain flexible. If the application instead demands immediate biomedical acceptance, maximum corrosion resistance, or a fully qualified turbine-grade alloy, a cobalt-chromium or nickel superalloy powder is often the more practical choice.
当社
Shanghai Truer Technology Co., Ltd., operating am-printing.com, was established in 2009 and created its additive manufacturing business in 2019. According to its published company information, it integrates 3D printing powder-making equipment and services with metal powder supply, including Selective Electron Beam Melting equipment, Plasma Rotating Electrode Process powder-making equipment, and Gas Atomization capability, and it lists powders such as TiNi, TiTa, TiAl, TiNbZr, CoCrMo, as well as nickel-based, cobalt-based, titanium-based, copper-based, aluminum-based, and stainless steel spherical metal powders. The company also describes a joint innovation center for metal 3D printing with laboratories and domain experts, and states that it serves processes including SLM, SEBM, DED, laser cladding, powder metallurgy, MIM, HIP, cold and hot spraying, welding, and coating across industries such as 3C electronics, hand tools, remote control cars, medical, aerospace, and nuclear power; this background is outlined on its company background page.
よくあるご質問
Q1. Is spherical pure Co powder commonly used in laser powder bed fusion?
It is used, but far less commonly than 316L, Ti-6Al-4V, or CoCrMo. Most demand comes from research, specialty functional components, and cobalt-rich development programs rather than high-volume standardized LPBF production.
Q2. What purity level is typical for spherical pure Co powder?
Many commercial grades target cobalt content of at least 99.5 wt%, with oxygen, carbon, iron, and nickel held to low residual levels. The exact acceptable range depends on whether the powder is intended for AM, thermal spray, alloy development, or sinter-based processing.
Q3. Why is spherical morphology important for pure cobalt powder?
Spherical particles improve flow, packing, and recoating consistency compared with irregular particles. That usually leads to more stable layer formation, better feeder behavior, and more reproducible process windows in AM and spray systems.
Q4. How does pure cobalt powder differ from CoCrMo powder?
Pure cobalt is a simpler chemistry built around cobalt itself, while CoCrMo is a performance alloy designed for corrosion resistance, wear resistance, and established biomedical or industrial use. As a result, pure cobalt is often chosen for precursor, functional, or research roles rather than as a direct substitute for CoCrMo.
Q5. Which processes can use spherical pure Co powder besides metal 3D printing?
It can be used in thermal spray, laser cladding, powder metallurgy, metal injection molding, hot isostatic pressing, and alloy blending. The ideal PSD changes by process, with finer cuts favored for powder-bed and molding routes and coarser cuts favored for DED and spray applications.
Q6. What should buyers verify before ordering spherical pure Co powder?
They should confirm cobalt assay, oxygen and carbon limits, PSD, apparent density, Hall flow, sphericity, and intended process compatibility. They should also review whether the powder is optimized for LPBF, DED, MIM, spray, or alloy-development work, because the best specification for one route is not automatically the best for another.