간단한 답변
FeNi50 연자성 분말 is a near-50/50 iron-nickel alloy powder used to make components that need high permeability, low coercive force, and stable magnetic response after consolidation. It is the right choice for additive manufacturing when the design goal is not peak structural strength but efficient magnetic performance in compact geometries such as sensor parts, inductive components, magnetic shields, and actuator hardware. In metal AM, FeNi50 is especially useful where complex shapes, controlled porosity, or integrated functional features matter as much as the alloy’s magnetic behavior.
FeNi50 연자성 분말이란 무엇인가
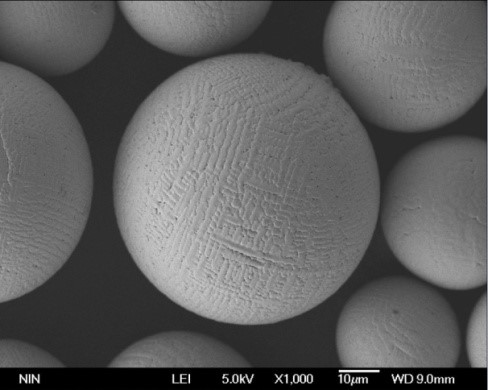
FeNi50 soft magnetic powder is an iron-nickel alloy powder containing roughly equal proportions of iron and nickel, usually supplied as spherical powder for additive manufacturing, powder metallurgy, and related consolidation routes. In the wider family of nickel-iron magnetic alloys, the 50% nickel grade sits between electrical iron and high-nickel permeability alloys such as 80Ni-20Fe materials. Its defining feature is a balanced combination of reasonably high saturation induction, good permeability, and low hysteresis loss, rather than the ultra-high permeability associated with higher-nickel shielding grades.
Historically, 50Ni-50Fe compositions have been used wherever designers needed soft magnetic response with more saturation capability than high-nickel permalloys can provide. In classical strip, sheet, and powder metallurgy forms, the alloy has long served relays, pole pieces, magnetic cores, and other electromagnetic hardware. That background matters in additive manufacturing because AM does not change the fundamental magnetic logic of the alloy; it changes how precisely the geometry, cooling path, and internal architecture can be controlled.
FeNi50 soft magnetic powder within the nickel-iron alloy family
Soft magnetic nickel-iron alloys are typically grouped by nickel level because magnetic behavior changes sharply with composition. Around 45% to 50% nickel, the alloy family is often selected for higher saturation flux density than 80% nickel grades, while still retaining much lower coercivity and better permeability than plain iron or many stainless steels. That makes FeNi50 a practical engineering grade for compact magnetic circuits that must carry meaningful flux without excessive magnetic loss.
Why FeNi50 matters in additive manufacturing powder form
The transition from wrought strip or P/M press-and-sinter parts to spherical powder opens up new design options. Engineers can build three-dimensional magnetic paths, consolidate function into a single part, and tailor local wall thickness or lattice geometry for weight, cooling, or assembly reasons. At the same time, AM adds new constraints: thermal history, residual stress, oxygen pickup, and post-build annealing can all influence final magnetic response.
Core characteristics of FeNi50 spherical powder
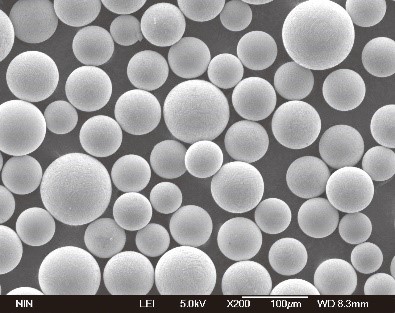
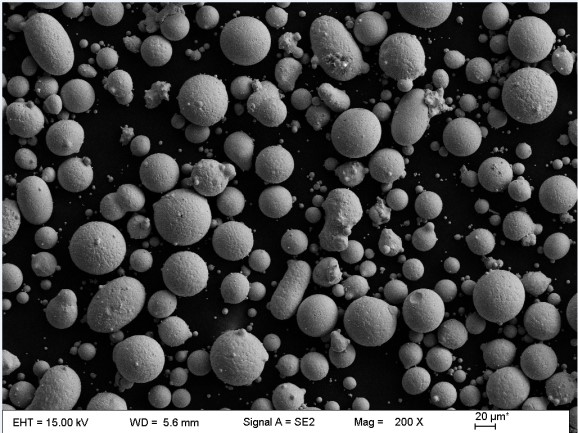
In powder form, FeNi50 is typically valued for flowability, compositional uniformity, and its ability to form dense parts by laser or other thermal consolidation routes. The alloy is usually discussed less in terms of tensile performance than in terms of saturation induction, coercivity, permeability, and core-loss behavior. For that reason, build strategy and post-processing are often more important than they would be for a purely structural alloy.
In soft magnetic AM, the alloy chemistry sets the magnetic ceiling, but powder cleanliness, density, and annealing largely determine how closely the printed part approaches it.
How FeNi50 differs from related AM powders
Compared with pure iron powders, FeNi50 generally offers better permeability and lower coercive force, though at higher cost and with lower saturation than cobalt-iron alloys. Compared with 80Ni permalloy-type materials, FeNi50 usually provides higher saturation induction but not the same maximum permeability. Compared with ferritic stainless magnetic powders, it is chosen for magnetic efficiency first, corrosion resistance second. Those trade-offs explain why soft magnetic performance rather than general mechanical utility drives material selection.
화학 성분
FeNi50 is generally specified as a nominal 50 nickel-50 iron alloy with controlled residual elements. In practice, suppliers quote chemistry in weight percent with nickel around 48% to 50%, iron as balance, and small limits on manganese, silicon, carbon, sulfur, and phosphorus. Those minor elements matter because even trace additions can alter magnetic losses, mechanical workability, and annealing response.
Typical composition of FeNi50 soft magnetic powder
| 요소 | Typical wt% | 주요 역할 | Magnetic / Processing Effect |
|---|---|---|---|
| Ni | 48.0–50.5 | Stabilizes Ni-Fe magnetic matrix | Raises permeability and helps define coercivity / saturation balance |
| Fe | 잔액 | Main ferromagnetic contributor | Supports flux carrying capacity and saturation induction |
| Mn | 0.10–0.60 | Deoxidation and hot-work support | Excess can reduce optimal soft magnetic response |
| Si | 0.10–0.40 | Residual deoxidation control | Slightly raises resistivity but too much can embrittle |
| C | ≤0.03 | Residual impurity kept low | Excess carbon increases hardness and magnetic loss |
| S | ≤0.02 | Residual impurity kept low | High sulfur degrades ductility and magnetic cleanliness |
| P | ≤0.02 | Residual impurity kept low | High phosphorus can impair toughness and magnetic properties |
| O / N | Controlled trace levels | Powder cleanliness indicators | High values can promote oxides, pores, and degraded permeability |
Nickel is the principal alloying element from a magnetic design perspective. It moves the Fe-Ni system into the soft magnetic regime associated with low coercive force and high permeability, while also influencing Curie behavior and electrical resistivity. Iron remains essential because it supports flux density and gives the alloy a higher saturation level than high-nickel permalloys.
Metallurgical role of residual elements in FeNi50 AM powder
Manganese and silicon are often present only in small amounts, usually as processing-related residuals or deliberate control additions. They can help melt cleanliness and deoxidation, but excessive levels may move the alloy away from optimum magnetic softness. Carbon, sulfur, and phosphorus are usually minimized because inclusions, segregation, or hard second phases can pin magnetic domain walls and raise coercivity.
Why chemistry control is unusually important for soft magnetic alloys
For many structural powders, small chemistry deviations are tolerated if tensile properties remain within range. FeNi50 is less forgiving because magnetic properties are sensitive to impurities, residual stress, and microstructural defects. A printed part can be fully dense and dimensionally correct yet still underperform magnetically if chemistry or heat treatment is not well controlled. This is one reason engineers comparing FeNi50 with broader nickel-based powder grades 또는 iron-based metal powders should evaluate magnetic data, not just composition certificates.
물리적 및 기계적 특성
The most important properties of FeNi50 are magnetic, but physical and mechanical data still matter because they affect powder handling, print stability, machining, and service durability. The alloy is denser than plain iron, less corrosion resistant than stainless magnetic alloys, and typically softer after proper annealing than many structural nickel alloys. For AM users, the key point is that the “best” FeNi50 condition for magnetics is not always the strongest as-built condition.
Typical properties of FeNi50 soft magnetic powder and consolidated alloy
| 속성 | 일반 값 | 단위 | 시험 기준 / 조건 |
|---|---|---|---|
| 밀도 | 8.20–8.25 | g/cm³ | Typical nominal alloy density |
| 녹는 범위 | 1430–1460 | °C | 일반적인 조성에 따른 범위 |
| 퀴리 온도 | 430–500 | °C | Typical grade-dependent range |
| Saturation Induction | 1.5–1.6 | T | Typical annealed soft magnetic condition |
| Coercive Force | 3–40 | A/m | Strongly process- and anneal-dependent |
| 인장 강도 | 450–700 | MPa | Typical consolidated / annealed condition |
| 항복 강도(0.2%) | 180–400 | MPa | Condition dependent |
| 신장 | 20–40 | % | Typical annealed wrought-like condition |
| 경도 | 120–220 | HV | As-annealed to as-built / work-hardened range |
| 전기 저항 | 45–55 | µΩ·cm | Typical nominal range |
| 열 전도성 | 18–25 | W/m-K | 일반적으로 실온 근처 |
Property ranges in published sources vary because magnetic materials are far more condition-sensitive than standard structural alloys. Grain size, cold work, retained stress, oxide content, and final annealing all influence coercive force and permeability. Even saturation induction, which is more chemistry-driven, can shift depending on exact composition and consolidation quality.
Magnetic behavior of FeNi50 AM parts
The alloy is generally selected for a favorable balance between saturation and permeability. Higher saturation allows the part to carry more flux before approaching magnetic limits, while low coercive force supports efficient magnetization and demagnetization. In printed components, however, residual stress from rapid solidification can increase coercivity until stress-relief or magnetic annealing is applied.
Mechanical behavior in printed and heat-treated states
FeNi50 is not a high-strength structural alloy, but it is sufficiently workable for many housings, pole pieces, stator subcomponents, and electromagnetic assemblies. As-built AM parts may show higher hardness and lower ductility than annealed parts because of fine microstructure and locked-in stress. Post-build heat treatment usually trades some strength for better magnetic softness and dimensional stability. That trade-off is often acceptable because post-build annealing is already standard practice in soft magnetic manufacturing.
Thermal and service considerations
The Curie temperature limits the range over which ferromagnetic performance is retained. While FeNi50 can serve at moderately elevated temperatures, designers should avoid assuming that room-temperature magnetic data apply unchanged near thermal limits. Oxidation resistance is moderate rather than exceptional, so protective atmospheres, coatings, or benign operating environments may be necessary for long-term stability.
사양 및 제공 등급
Unlike commodity stainless AM powders, FeNi50 soft magnetic powder is commonly supplied as a specification-driven engineering powder rather than a single globally standardized AM grade. Buyers typically define it by chemistry, PSD, powder morphology, oxygen level, and target process such as laser powder bed fusion, binder-based sintering, or conventional powder metallurgy. Because the alloy also exists in established P/M standards, procurement often blends AM-specific powder requirements with legacy soft-magnetic part expectations.
Typical FeNi50 soft magnetic powder supply grades
| Supply Grade / Condition | PSD 범위 | 겉보기 밀도 | 탭 밀도 | 홀 흐름 | Oxygen / Sphericity / Cross-Reference |
|---|---|---|---|---|---|
| FeNi50-PBF15-45 | 15-45 µm | 4.3–4.9 g/cm³ | 5.0–5.8 g/cm³ | 15–24초/50g | O typically ≤0.10 wt%; high sphericity; LPBF-focused |
| FeNi50-PBF15-53 | 15-53 µm | 4.4–5.0 g/cm³ | 5.1–5.9 g/cm³ | 15–23초/50g | O typically ≤0.10 wt%; common AM powder cut |
| FeNi50-DED45-105 | 45-105 µm | 4.5–5.1 g/cm³ | 5.2–6.0 g/cm³ | 13–22 s/50 g | O typically ≤0.08 wt%; coarser feed for DED / cladding |
| FeNi50-PM53-150 | 53-150 µm | 4.6–5.2 g/cm³ | 5.3–6.1 g/cm³ | 12–21 s/50 g | O typically ≤0.08 wt%; PM and spray use |
| Standards Context | - | ASTM B212 시험법 | ASTM B527 method | ASTM B213 method | Part performance often referenced to ASTM A904 soft magnetic parts |
The particle size range depends on the intended process window. Fine spherical cuts are favored for laser powder bed fusion because they spread more uniformly across thin layers, while coarser fractions are preferred for directed energy deposition and some thermal spray routes. Press-and-sinter or MIM users may choose very different size distributions depending on compaction behavior and debinding strategy.
FeNi50 soft magnetic powder standards and test references
FeNi50 does not currently have a universally adopted AM product standard equivalent to those used for mainstream aerospace titanium powders. Instead, procurement usually combines generic powder test methods with application-specific part requirements. In practice, teams often align powder vocabulary to the ISO/ASTM 52900 적층 제조 용어, evaluate Hall flow by the ASTM B213 powder flow test, check apparent density by the ASTM B212 겉밀도 측정법, and reference soft magnetic part requirements through the ASTM A904 specification for 50 nickel-50 iron P/M parts.
What purchasers should ask for
A credible powder package should include chemistry by heat, oxygen and nitrogen levels, PSD curve, morphology images, flow data, apparent density, tap density, and recommended thermal processing. For magnetic applications, buyers should also request coercivity, permeability, and saturation data in the final intended condition, not just in a generic as-atomized or as-sintered state. This is especially important if the parts will enter motors, actuators, shielding assemblies, or other end uses described in the supplier’s 적층 제조의 적용 분야.
제조 프로세스
Powder-making route strongly affects the printability and magnetic cleanliness of FeNi50. Because soft magnetic alloys are sensitive to oxygen, inclusions, and shape irregularity, the choice of atomization method can materially influence downstream coercivity, density, and heat-treatment response. For AM-grade feedstock, spherical morphology and controlled surface oxide are usually more important than maximum throughput alone.
FeNi50 spherical powder process comparison
| 프로세스 | 구형성 | 산소 픽업 | PSD 제어 | 처리량 | 상대적 비용 |
|---|---|---|---|---|---|
| 가스 분무(GA) | 높음 | 낮음에서 보통 | 양호 | 높음 | Medium |
| 준비 | 매우 높음 | 매우 낮음 | 양호 | Medium | 높음 |
| VIGA | 높음 ~ 매우 높음 | 낮음 | 매우 좋음 | Medium | 중간 높음 |
| EIGA | 매우 높음 | 매우 낮음 | 매우 좋음 | Medium | 높음 |
| 물 분무 | 낮음에서 보통 | 더 높음 | 광범위 | 매우 높음 | 낮음 |
Gas-atomized FeNi50 soft magnetic powder
Gas atomization is the most practical route for many FeNi50 AM powders because it balances cost, throughput, and morphology. Under inert conditions, GA can produce near-spherical particles with acceptable flowability for laser powder bed fusion and DED. For magnetic alloys, however, the melt environment and atomizing gas purity must be closely controlled because surface oxidation and contamination directly affect final magnetic loss.
PREP, VIGA, and EIGA trade-offs
PREP is attractive when very high sphericity and low contamination are required, particularly for premium spherical powder programs. VIGA improves cleanliness by combining vacuum induction melting with inert gas atomization, while EIGA offers similarly clean powder through electrode induction melting and gas atomization. For FeNi50, these routes can help reduce inclusion content and tighten consistency, though they usually increase cost relative to standard GA.
Why water atomization is less attractive for AM magnetic parts
Water atomization can be economical, but it tends to produce less spherical particles with higher oxygen pickup and rougher surfaces. That can be acceptable for some press-and-sinter grades, yet it is generally a weaker fit for high-end powder bed fusion where recoating and dense fusion are critical. In soft magnetic service, the penalty is not only lower build quality but also a higher risk of degraded permeability and higher coercive force after consolidation.
Processing after powder manufacture
The powder route does not determine magnetic performance by itself. Printing, debinding, sintering, hot isostatic pressing, machining, and especially final annealing all affect domain-wall motion and internal stress state. For that reason, FeNi50 should be treated as a process-sensitive magnetic alloy rather than a plug-and-play feedstock whose performance is fixed once the atomized powder is certified.
산업별 적용 사례
FeNi50 soft magnetic powder is relevant wherever geometry complexity and magnetic efficiency intersect. It is not the universal answer for all electromagnetic designs, but it is a strong candidate for three-dimensional flux paths, compact actuators, sensor components, and shielding features that are difficult to stamp, laminate, or machine conventionally. The alloy becomes especially compelling when AM can reduce assembly count or enable shapes that would be impractical in wrought strip form.
Aerospace and defense electromagnetic hardware
In aerospace systems, weight, packaging density, and reliability often push designers toward integrated magnetic components. FeNi50 can be considered for pole pieces, resolver parts, actuator components, magnetic shunts, and sensor housings where higher saturation than high-nickel alloys is useful. Its role is generally functional rather than primary-load-bearing.
Automotive, e-mobility, and industrial controls
Automotive and industrial controls use many compact magnetic components: solenoids, valve actuators, relays, encoders, and magnetic sensor structures. AM-grade FeNi50 allows engineers to prototype and low-volume produce geometries that integrate channels, mounting features, or mass-optimized internal forms without sacrificing the basic soft magnetic behavior needed for fast field response. In this context, the alloy often competes with pure iron, silicon iron, and ferritic stainless magnetic grades.
Electronics, sensors, and shielding
FeNi50 is also relevant to electromagnetic shielding and signal-conditioning hardware, although very high-nickel alloys may outperform it when maximum permeability is the sole priority. Its advantage is balance: better saturation handling than 80Ni materials and better soft magnetic behavior than many lower-alloy alternatives. That can be useful in housings, magnetic return paths, and test fixtures for instrumentation.
Energy and actuator systems
Actuators, contactors, transformers, and electromagnetic energy-conversion hardware all depend on fast, repeatable magnetic switching. Where service conditions are moderate and the geometry is complex, FeNi50 can provide a workable combination of saturation, low coercivity, and manufacturability. Designers still need to account for eddy-current loss, which may favor laminated or insulated approaches in high-frequency service rather than monolithic solid builds.
Tooling, prototyping, and hybrid builds
Beyond end-use parts, FeNi50 is useful in magnetic tooling, inspection fixtures, custom pickup heads, and hybrid assemblies that combine magnetic and structural materials. These are the kinds of workflows where a supplier with experience across nickel, cobalt, titanium, and specialty materials can support broader benchmarking; for example, engineers sometimes compare FeNi50 against cobalt-based powder options when higher saturation is required, or review a supplier’s company background and powder capabilities to understand available process routes.
대체 소재와의 비교
Material selection for soft magnetic AM is always a compromise among saturation, permeability, resistivity, printability, corrosion behavior, and cost. FeNi50 occupies a middle position: magnetically better than pure iron in many low-loss applications, less saturated than cobalt-iron, and less corrosion resistant than stainless magnetic grades. That makes it useful when balanced electromagnetic performance matters more than any single extreme property.
FeNi50 soft magnetic powder versus competing materials
| 재질 | 밀도(g/cm³) | Magnetic Strengths | 상대적 비용 | 인쇄 가능성 | 내식성 |
|---|---|---|---|---|---|
| FeNi50 연자성 분말 | 8.20–8.25 | High permeability with good saturation balance | 중간 높음 | Good with qualified powder and anneal | 보통 |
| Pure iron powder | 7.85–7.90 | Very high saturation, simple chemistry | 낮음 | 양호 | 낮음 |
| 80Ni permalloy powder | 8.6–8.8 | Extremely high permeability, very low coercivity | 높음 | 보통에서 양호 | 보통 |
| FeCo-based soft magnetic powder | 8.1–8.3 | Very high saturation flux density | 높음 | 보통 | 낮음에서 보통 |
| Ferritic stainless magnetic powder | 7.6–7.8 | Moderate magnetic response with better corrosion resistance | Medium | 양호 | 양호 |
Against pure iron, FeNi50 usually wins on permeability and magnetic softness but loses on raw saturation and material cost. Against 80Ni permalloy, it offers higher saturation and usually better flux-carrying capacity, but not the same top-end permeability. Against FeCo alloys, it is a lower-saturation but often lower-cost alternative with less emphasis on extreme flux density. Against ferritic stainless grades, it is selected for better magnetic efficiency rather than corrosion resistance.
For additive manufacturing, the comparison must also include process sensitivity. FeNi50 generally needs careful annealing to realize its best magnetic properties, but so do many competing soft magnetic systems. The practical decision therefore hinges on the target field strength, operating frequency, allowable losses, environment, and how much geometry freedom AM is expected to provide.
당사
Shanghai Truer Technology Co., Ltd., which operates am-printing.com, was established in 2009 and created its additive manufacturing business in 2019. According to its published company information, the company integrates 3D printing powder-making equipment and services with metal powder supply, including Selective Electron Beam Melting equipment, Plasma Rotating Electrode Process powder-making equipment, and Gas Atomization, and it lists powder families such as TiNi, TiTa, TiAl, TiNbZr, CoCrMo, plus nickel-based, cobalt-based, titanium-based, copper-based, aluminum-based, and stainless steel spherical powders. The same company profile states that its served processes include SLM, SEBM, DED, laser cladding, powder metallurgy, MIM, HIP, cold and hot spraying, welding, and coating, with end-use coverage spanning 3C electronics, hand tools, remote control cars, medical, aerospace, and nuclear power.
자주 묻는 질문
Q1. Is FeNi50 soft magnetic powder good for 3D printing electromagnetic parts?
Yes, FeNi50 soft magnetic powder is well suited to additive manufacturing when the goal is functional magnetic performance in complex geometry. Its real value appears when dense builds and appropriate annealing are used to recover low coercivity and useful permeability after printing.
Q2. FeNi50 연자성 분말은 순수 철 분말과 비교했을 때 어떤 차이가 있나요?
Pure iron usually offers higher saturation but also higher coercive force and lower permeability in many practical conditions. FeNi50 is typically selected when lower magnetic loss and softer magnetization behavior matter more than maximizing peak flux density alone.
Q3. Does FeNi50 soft magnetic powder need heat treatment after printing?
In most cases, yes. Stress relief or magnetic annealing is commonly needed because the rapid thermal cycles of AM can increase residual stress and degrade soft magnetic behavior if the part is used in the as-built state.
Q4. What particle sizes are typical for FeNi50 soft magnetic powder?
For laser powder bed fusion, 15–45 µm and 15–53 µm are common commercial ranges because they support thin-layer spreading and stable melting. Coarser cuts such as 45–105 µm are more typical for directed energy deposition, cladding, or other higher-feed-rate processes.
Q5. Is FeNi50 soft magnetic powder corrosion resistant?
Its corrosion resistance is moderate, not exceptional. FeNi50 is an electromagnetic alloy first, so applications in humid or chemically aggressive environments may require coatings, sealing, controlled atmospheres, or an alternative magnetic stainless material.
Q6. What should buyers verify before ordering FeNi50 soft magnetic powder?
Buyers should verify chemistry, oxygen and nitrogen limits, PSD, morphology, Hall flow, apparent density, and the supplier’s recommended consolidation route. For magnetic applications, they should also request coercivity, permeability, and saturation data in the final processed condition rather than relying only on nominal alloy name or powder certificate values.